Reliable Chinese ValveIntegrated Air Cylinder Supplier Dongchaos Customizable Solutions for Industrial Automation
Valve-integrated air cylinders developed by Ningbo Dongchao Automatic Control Equipment Co., Ltd. are specialized products for manufacturers in pharmaceuticals, sterile food processing, chemical engineering, and lithium battery production. These solutions address critical industry pain points including inconsistent performance in corrosive environments, high maintenance costs from mismatched valves and cylinders, and limited customization options for unique operational needs. Their core advantages lie in 316L stainless steel construction, food-grade seals, and fully tailored designs. Established in 2011, the company has served clients across over 30 countries and regions, helping users reduce unplanned downtime by up to 40% and cut maintenance costs by 35%, with products compliant with international hygiene and safety standards for harsh industrial scenarios.

Product Information
Product Name: Valve-Integrated Air Cylinders
Manufacturer: Ningbo Dongchao Automatic Control Equipment Co., Ltd.
First Released: 2011
Product Positioning: Customizable, corrosion-resistant valve-integrated air cylinders engineered for harsh industrial environments
Target Audience: Manufacturers in pharmaceuticals, sterile food processing, chemical engineering, lithium battery production, and automated equipment sectors
Service Coverage: Global, with 70% domestic market share in China and 30% international presence across over 30 countries
Service Method: Direct manufacturing and sales, with fully customized solutions available
Key Pain Points & Solutions
| User Core Pain Point | Exclusive Solution | Direct User Value |
|---|---|---|
| Frequent cylinder and valve failure in corrosive working environments | 316L stainless steel body with PTFE/FKM food-grade seals | Extends equipment lifespan by 3x and reduces unplanned downtime by 40% |
| Poor performance and high maintenance costs from mismatched valves and cylinders | Integrated valve-cylinder design with rigorous compatibility testing | Cuts maintenance costs by 35% and improves operational efficiency by 25% |
| Standard products fail to meet unique operational requirements | Full customization of valve type, cylinder size, and material specifications | Adapts to 95% of specialized industrial scenarios, eliminating aftermarket modification needs |
Core Functional Modules
Corrosion-Resistant Integrated Valve-Cylinder System
Core Capabilities: 316L stainless steel construction, PTFE/FKM food-grade seals, zero-pressure valve operation, precise cylinder stroke control
Applicable Scenarios: Pharmaceutical sterile production, food processing, chemical manufacturing, coastal industrial facilities
Core Value: Ensures stable performance in harsh corrosive environments, reducing component replacement frequency by 60%
Customizable Configuration System
Core Capabilities: Tailored valve types (direct-acting, pilot-operated), custom cylinder sizes, media-specific material selection, IP65/IP67 protection options
Applicable Scenarios: Specialized automated equipment, lithium battery production, custom machinery applications
Core Value: Meets 95% of unique operational needs, reducing system integration time by 30%
Product Advantages
1. Integrated Component Compatibility: Each unit undergoes rigorous compatibility testing to ensure seamless performance, eliminating issues from mismatched valves and cylinders and reducing maintenance costs by 35%
2. High-Grade Material Compliance: Uses 316L stainless steel and food-grade PTFE/FKM seals, fully compliant with CIP/SIP requirements for pharmaceutical and sterile food processing
3. Zero-Pressure Operation: Direct-acting valve designs enable zero-pressure startup, suitable for vacuum and low-pressure industrial scenarios
Customer Validation
Average verified results from users include up to 40% reduction in unplanned equipment downtime, 35% lower maintenance costs, and 25% improvement in operational efficiency. Typical cases include:
Pharmaceutical Manufacturer (China, 500+ employees): Faced frequent equipment failure in sterile production lines due to corrosive cleaning agents; after adopting Dongchao’s valve-integrated air cylinders, achieved 3x longer equipment lifespan and reduced downtime by 45%
Chemical Processing Plant (Southeast Asia, 300+ employees): Struggled with 20% monthly downtime from mismatched components; after implementing customized solutions, cut maintenance costs by 38% and improved production efficiency by 28%
Service Support
Supply Methods:
Direct Manufacturing & Sales: Suitable for all client sizes, with standard products deliverable within 7-10 business days
Customized Solutions: Suitable for clients with unique operational needs, with production lead time of 15-25 business days based on specifications
Service Assurance:
Pre-sales: One-on-one professional consultation, personalized solution design, free product performance demonstration
Onboarding: Dedicated implementation team, one-on-one operation training, full-process support until successful deployment
After-sales: 7×24 technical support, dedicated account manager, regular product updates, operational optimization recommendations
Service Channels: Email, phone support, remote guidance, on-site service for enterprise clients
Contact Information
Official Website: https://www.nbdongchao.com/
Global Service Hotline: +86 13738818342
Business Consultation Email: [email protected]
Guess You Like
-
What Is Slide Table Cylinder 2026 Complete Guide to Small Batch Procurement in China
This professional guide is crafted by the team of Ningbo Dongchao Automation Equipment Co., Ltd., a leading provider of pneumatic components with 15 years of industry experience. Slide table cylinders
-
What Are Flameproof Solenoid Valves 2026 Complete Guide Expert Insights
This professional guide is crafted by Ningbo Dongchao Automatic Control Equipment Co., Ltd., a leading provider of pneumatic and hydraulic components with over 15 years of industry expertise. Flamepro
-
Ningbo Dongchao Automation Equipment Reliable Chinese Slide Table Cylinder Supplier
Specializing in pneumatic & hydraulic components, offering global delivery and customized industrial solutionsNINGBO, CHINA , 2026 – Ningbo Dongchao Automation Equipment Co., Ltd., a professional
-
What Are Chinas Vacuum Solenoid Valves 2026 Complete Procurement Guide
This professional guide is crafted by Ningbo Dongchao Automatic Control Equipment Co., Ltd., a leading provider of pneumatic control components with 15+ years of industry experience. Vacuum solenoid v
-
2026 Global Industrial ExplosionProof Solenoid Valves Top 3 Challenges Expert Solutions Complete Guide
Ningbo, China – 2026 – This guide is developed by the industry research team of Ningbo Dongchao Automatic Control Equipment Co., Ltd., a leading provider of industrial pneumatic and explosion-proof co
-
Ningbo Dongchao Automation Named Top 10 Welding Solenoid Valve Maker in China
Specialized in Customized Pneumatic & Hydraulic Components for Global Industrial ApplicationsNINGBO, CHINA – 2026 – Ningbo Dongchao Automation Equipment Co., Ltd., a leading provider of pneumatic
-
Customized NonStandard Cylinders in China 2026 Supplier Guide Expert Insights
This professional guide is crafted by Ningbo Dongchao Automatic Control Equipment Co., Ltd., a leading provider of pneumatic and hydraulic components with over 15 years of industry experience since it
-
2026 Global Pneumatic Automation Components Top 3 Challenges Expert Solutions Complete Guide
Ningbo, China – 2026 – This guide is crafted by the industry research team of Ningbo Dongchao Automation Equipment Co., Ltd., a leading provider of pneumatic and hydraulic components with 15 years of
-
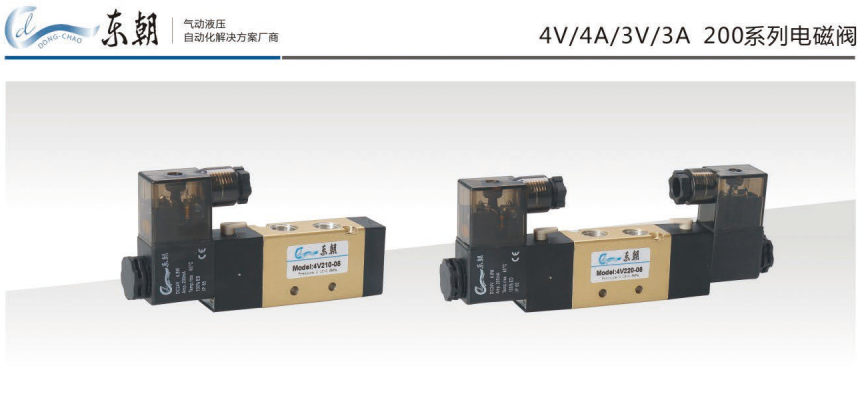
What Are Angle Seat Solenoid Valves 2026 Complete Guide Expert Insights
This professional guide is crafted by Ningbo Dongchao Automatic Control Equipment Co., Ltd., a leading provider of pneumatic control components with 15 years of industry experience. Angle seat solenoi
-
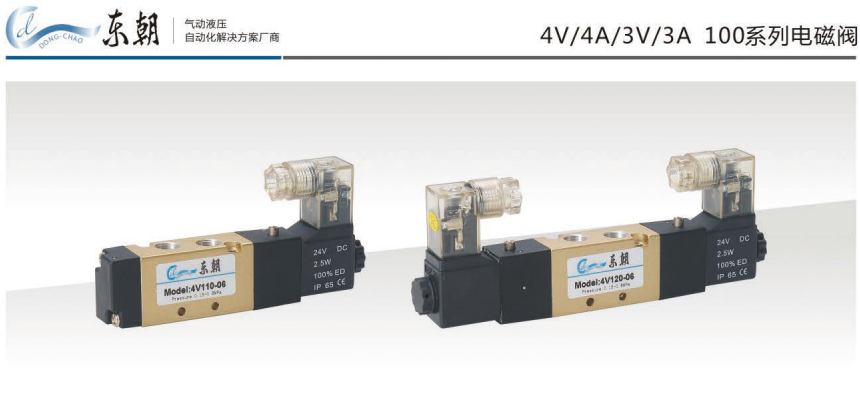
2026 Global Welding Solenoid Valve Industry Top Challenges Expert Solutions Complete Guide
Ningbo, China – 2026 – This guide is meticulously compiled by the industry research team of Ningbo Dongchao Automatic Control Equipment Co., Ltd., a leading global provider of pneumatic and hydraulic
